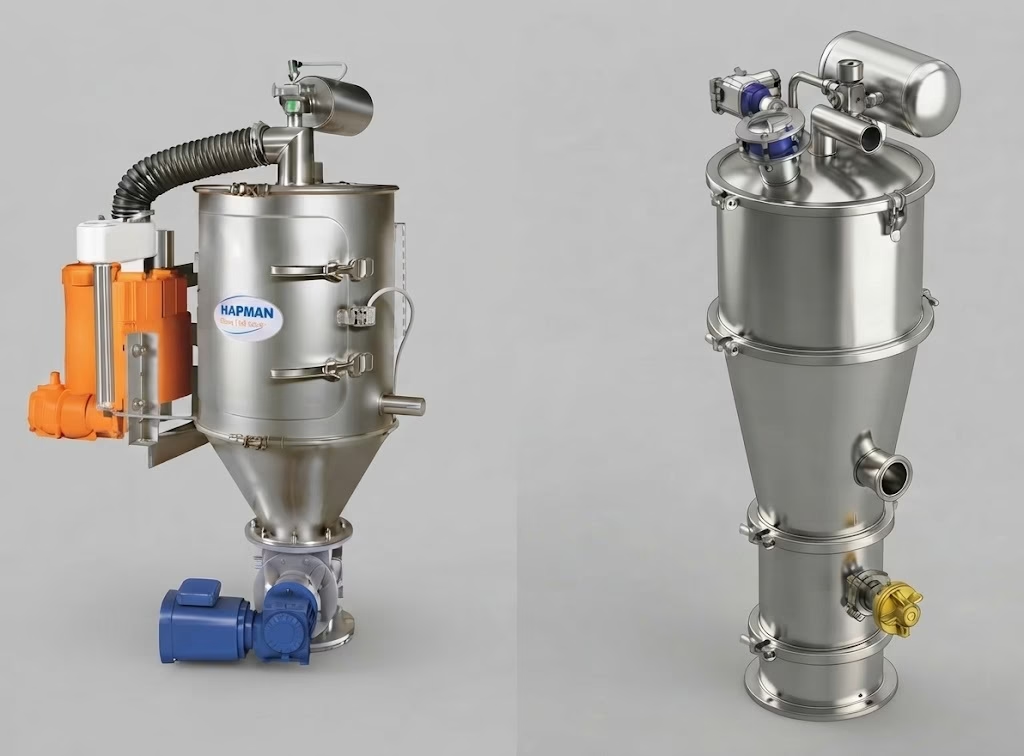
A vacuum conveyor is a type of pneumatic conveying system that uses a vacuum to move bulk materials such as powders, granules, and other dry materials through an enclosed pipeline. By creating a pressure difference, the conveyor gently pulls the materials from one location to another, ensuring a dust-free and hygienic transfer process.
These conveyors are widely used in industries like food processing, pharmaceuticals, and chemicals due to their ability to maintain high sanitary standards and prevent contamination. They are also known for their compact, space-saving design, flexible installation options, and efficient material transfer capabilities.
| Industry Segment | Target Materials | Processing Solution |
|---|---|---|
| Food & Beverage | Flour, Sugar, Spices, Grain, Starch | Batch dosing, sanitary packaging feed, dust-free transfer |
| Pharmaceutical | API, Granules, Fine Powders, Capsules | Tablet press feeding, cleanroom transfer, GMP compliance |
| Chemical Processing | Pigments, Resins, Toxic Powders, Catalysts | Reactor loading, hazardous material containment, blending |
| Plastics & Polymer | Pellets, Additives, Regrind, Flakes | Extruder loading, injection molding supply, pellet conveying |
| Agriculture & Feed | Seeds, Fertilizers, Mineral Supplements | Automated silo filling, bulk material distribution |
Traditional mechanical conveying systems can be bulky, messy, and high-maintenance. Our industrial vacuum conveyors solve these pain points by offering a completely enclosed, dust-free pipeline that guarantees a hygienic environment for food, pharmaceutical, and chemical processing.
Zero Contamination & Spillage: Fully enclosed system eliminates dust emissions and material loss during bulk solids transfer.
Drastically Reduced Downtime: Features fewer moving parts and tool-less side-door filter access for rapid cleaning between runs.
Maximize Floor Space: A compact, flexible design that easily maneuvers around corners, multiple levels, or tight ceiling spaces.
Simple, quiet, plug-in vacuum conveying for shorter runs and lighter duty.
Our compact series features an integral blower vacuum conveyor and regenerative blower pneumatic conveyor design, engineered for efficient powder and granule transfer in tight industrial spaces across Australia.
The workhorse for distance, volume, and continuous operation.
For heavy-duty plant requirements, our roots blower vacuum conveyor acts as a high-capacity pneumatic conveying system built for continuous operation and long distance vacuum conveying across Australia.
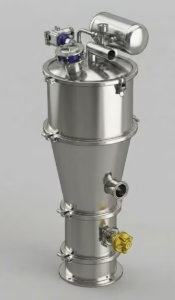
| Model | 16D | 16R | 20D | 20R | 24D | 24R | 30R |
|---|---|---|---|---|---|---|---|
| CAPACITY (m³/h)* | 0.48 | 0.60 | 1.02 | 1.26 | 2.40 | 2.70 | 3.84 |
| FILTER AREA (m²) | 1.21 | 1.21 | 1.21 | 1.21 | 2.88 | 2.88 | 5.76 |
| BLOWER SIZE (kW)** | 1.12 | 1.12 | 1.86 | 1.86 | 3.73 | 3.73 | 7.46 |
| COMPRESSED AIR REQ. (kPa) | 414 | 414 | 414 | 414 | 552 | 552 | 552 |
Note: Specifications subject to change without notice - Contact a factory sales engineer for specifications and options.
*Nominal capacity based upon 15.24 m equivalent length piping (50 ft).
**Larger blower sizes and configurations available.
| Model No. | Motor Power (kW) | Conveying Capacity (kg/h)* |
|---|---|---|
| NAP-1 | 1.5 | 400 |
| NAP-2 | 2.2 | 600 |
| NAP-3 | 3.0 | 1,200 |
| NAP-4 | 5.5 | 2,500 |
| NAP-6 | 5.5 | 3,200 |
| NAP-7 | 7.5 | 6,000 |
| NAP-10-6 | 7.5 | 6,000 (at 10 m distance) |
| NAP-20-5 | 11.0 | 5,000 (at 20 m distance) |
*Note: Conveying capacity measured using flour at a 4-meter conveying distance. Longer distances and material characteristics will alter performance.
Our industrial vacuum conveying systems are fully supported by Australian-based technicians and engineered for guaranteed compliance with Australian sanitary and safety standards, ensuring seamless integration into your local facility.
Selecting the right system depends on your material characteristics, airflow requirements, and suction stability. For continuous powder transfer or high-volume applications, we generally recommend our Roots Blower Series for its higher displacement and sustained filter performance under continuous duty. For shorter runs, fine powders, or tight installation spaces, our Compact Series offers a simpler, self-contained solution. If your process involves abrasive or hazardous materials, our team can help select a configuration that prioritises containment and easy washdown.
Not sure which model fits your facility? Our factory sales engineers are available to review your material specifications and provide a tailored recommendation.
Integrate the vacuum conveyors with other bulk material equipment from Noggrann, like the BULK BAG UNLOADER, TUBULAR DRAG CONVEYORS, FLEXIBLE SCREW CONVEYORS, BULK BAG FILLERS, or SCREW FEEDERS for a complete conveying system.
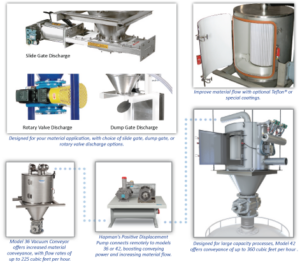
A vacuum conveyor is a pneumatic system that uses a negative pressure differential (a vacuum) generated by a pump or blower to draw bulk materials (powders, granules, tablets) from a source (e.g., drum, hopper) through a pipeline to a destination receiver.
Vacuum conveying is generally better for fine or difficult powders because it offers total dust containment, prevents product segregation, and is easier to clean, minimizing cross-contamination risks.
Key factors include the material's particle size and density, its abrasiveness and friability (fragility), the required throughput rate, and the conveying distance and height.
Primary advantages include superior dust control and product containment (as leaks flow inward), simpler pipeline routing, safer handling of combustible dusts, and the ability to convey materials from multiple pickup points to a single receiver.
Vacuum conveyors are standard in the Pharmaceutical (tablet and powder transfer), Food & Beverage (sugar, flour, spices), Chemical (resin, additives), and Plastics (pellets, granules) industries due to their hygienic and contained operation.
Yes, by utilizing dense phase conveying, the material is moved at lower velocities in "plugs," which significantly reduces particle breakage (fragile materials) and wear on the pipe and components (abrasive materials).
Blockages are usually caused by conveying material that is too moist or cohesive, or by exceeding the system's capacity. Prevention involves proper system sizing, maintaining adequate air velocity (especially in dilute phase), and using fluidizing or air-assist devices
Vacuum conveyors are considered fully contained systems. Because they operate under negative pressure, any small leak in the system results in air being drawn into the pipe, preventing product dust from escaping into the facility, thus providing superior dust control.
A regenerative blower creates airflow through a spinning impeller and is best suited to lower-vacuum, lower-flow applications — it's quiet, self-contained, and needs no separate blower room. A roots blower is a positive-displacement unit that pulls a deeper vacuum and moves a much higher volume of air, making it suited to longer distances and heavier, continuous-duty transfer.
We use regenerative blowers in our Compact Series — a plug-in, self-contained solution ideal for shorter distances, fine powders, and tight production spaces. Roots blowers power our High-Capacity Series, built for continuous, heavy-duty transfer over long-distance and cross-plant runs.