As a leading supplier, Noggrann Australia provides high-performance industrial agitators, tank agitators, and industrial mixers engineered specifically for reliable fluid blending.
Whether you require a crude oil blender, a chemical process mixer, a drilling mud agitator, or an explosion-proof mixing system, we can customize our range to match your exact tank geometry, viscosity levels, and process requirements. Furthermore, our heavy-duty configurations easily withstand the most demanding plant environments.
Designed for continuous operation in demanding environments, including abrasive mineral slurries and corrosive chemical tanks.
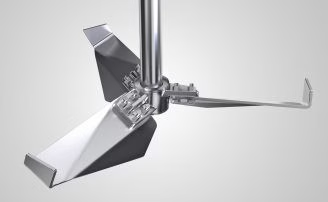
Available with axial-flow, radial-flow, high-shear and hydrofoil impellers to suit diverse mixing duties—from gentle blending to high-intensity dispersion.
Every industrial mixing system is tailored to tank size, slurry density, viscosity and process requirements for optimal performance.
Agitator mixer systems are widely used across:
Upstream Crude & Sludge Storage – Preventing solids deposition, maintaining homogeneity in crude oil storage tanks, and managing heavy BS&W (Basic Sediment and Water).
Refinery & Petrochemical Processing – High-intensity blending in reaction tanks, chemical dissolving, emulsification, and gasoline/distillate blending.
Drilling Mud & Slurry Fluids – Maintaining uniform density and suspending heavy weighting agents in active mud tanks and reserve pits.
Produced Water & Wastewater Treatment – Flocculation, oil-water separation setups, flash mixing, and chemical dosing in industrial environmental circuits.
See full impeller and SK-series specifications on our Industrial Mixing Agitators page.
Our industrial agitators cover a broad range of mixing duties:
Water treatment mixing for coagulation/flocculation
Crude oil blending and basic sediment suspension
Pharmaceutical emulsions and suspensions
The primary function of an oil and gas mud agitator is to maintain uniform fluid density and suspend heavy weighting agents (such as barite) within active mud tanks and reserve pits. Continuous mechanical agitation prevents solids from settling at the bottom of the tank, ensuring the drilling fluid retains its required rheological properties for wellbore stability and efficient cuttings transport. For reliable upstream operations, heavy-duty slurry mixers ensure consistent fluid homogeneity before the mud reaches downstream solid control systems.
Selecting the correct tank agitator configuration depends on the tank geometry, fluid viscosity, and specific mixing duties:
Industrial mixers utilized in oil refineries and petrochemical processing must feature robust engineering to operate safely in volatile atmospheres. Crucial compliance and safety features include:
Answer: The selection of the impeller directly determines whether a system delivers low-shear flow or high-intensity dispersion:
Answer: In critical environments like high-pressure reactors and sealed chemical tanks, mechanical failures are prevented by integrating advanced load-bearing structures. For instance, the Noggrann SK400 and SK500 series mixers use a true dry-well leak-proof structure paired with a rugged three-point bearing support system. This design isolates the drive gear oil from the process fluid, entirely eliminating oil contamination risks while absorbing the massive mechanical loads caused by turbulent fluid dynamics.