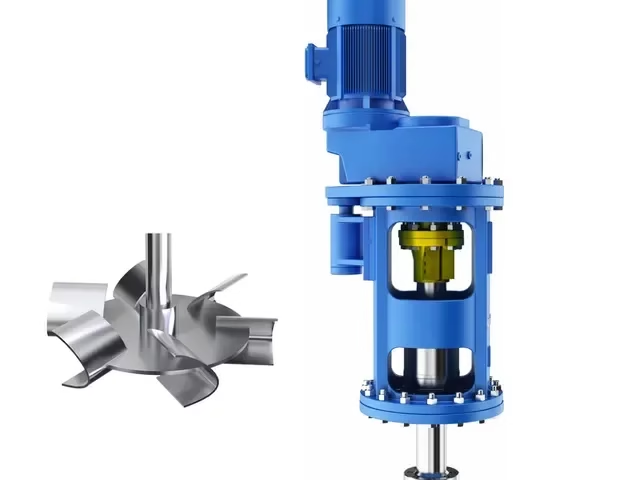
Noggrann Australia delivers heavy-duty industrial mixers and tank agitators engineered for harsh local operating conditions. Serving mining, chemical, and wastewater plants across Australia, our robust systems provide reliable blending with fast local support and OEM parts.
Furthermore, we customize our full product range to match your exact tank geometry, fluid viscosity levels, and process requirements. Whether you require a crude oil blender, a chemical process mixer, a drilling mud agitator, or an explosion-proof mixing system, our engineers provide precise guidance. Consequently, you receive an optimized mixing solution that fits your facility's layout perfectly. In addition, our robust designs minimize operational downtime.
Designed for continuous operation in demanding environments, including abrasive mineral slurries and corrosive chemical tanks.
Available with axial-flow, radial-flow, high-shear and hydrofoil impellers to suit diverse mixing duties—from gentle blending to high-intensity dispersion.
Every industrial mixing system is tailored to tank size, slurry density, viscosity and process requirements for optimal performance.
Agitator mixer systems are widely used across:
Mining & Minerals Processing – slurry mixing, leaching tanks, gold cyanidation.
Chemical & Petrochemical – reaction tanks, dissolving, emulsification.
Food & Beverage – milk, sauces, syrups, fermentation and flavour mixing.
Pharmaceutical & Cosmetics – creams, lotions, suspension mixing.
Water & Wastewater Plants – flocculation, aeration, chemical dosing.
Ideal for low-viscosity liquids, solid suspension and heat transfer in process tanks.
Suitable for high-shear applications such as emulsification, gas dispersion and particle breakup.
Designed for high-viscosity products, pastes and gels—perfect for cosmetics, adhesives and thick slurries.
Used for breaking down agglomerates, pigments and producing fine emulsions.
Our industrial agitators cover a broad range of mixing duties:
Slurry agitation tanks for minerals processing
Gold leaching agitators for cyanide leach circuits
Chemical blending and dissolving
Water treatment mixing for coagulation/flocculation
Food processing requiring hygienic stainless steel mixers
Pharmaceutical emulsions and suspensions
The SK400 series dynamic mixing agitator fulfills various industrial mixing needs under highly complicated conditions. Specifically, this line offers both top-entry and side-entry configurations with a motor power range from 0.37kW to 315kW and variable mixing speeds from 1 RPM to 400 RPM. Because we equip the unit with an advanced, true dry-well leak-proof structure and a rugged three-point bearing support system, the SK400 completely eliminates oil contamination risks. Therefore, it serves as a highly reliable selection for closed petrochemical tanks and storage vessels.
SK500 series reactor agitators are with high performance for extended lifetime, and reduced maintenance and operating costs. Types of agitators are used in reactors specially designed for the application of sealed vessel mixing.
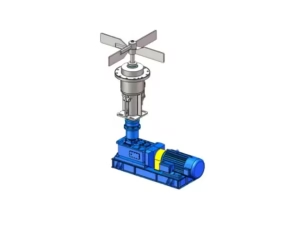
The SK600 series bottom-entry agitators provide reliable service and easily absorb massive mechanical loads in large-scale operations. In particular, these heavy-duty units optimize fluid turnover in high-strength processing environments. They easily handle high-viscosity petrochemical blending, heavy sludge waste treatment, and high-velocity gas dispersal applications. Additionally, this design serves as the ideal alternative when top-space on the pressure vessel is limited.
Australian supplier with industry-specific engineering guidance
Custom-built tank agitators with precise motor sizing
Durable construction for corrosive and abrasive applications
Fast lead times and OEM replacement capabilities
Solutions tailored for your actual tank volume, slurry density and process goals
Industrial agitators and mixers are widely used across various processing industries.
The primary purpose is to efficiently extract valuable metals from finely ground ore (slurry or pulp) by dissolving them in a chemical solvent. The agitator ensures constant, uniform contact between the solid ore particles and the liquid solvent, preventing the solids from settling at the bottom of the tank and maximizing the extraction rate.
The agitator uses a motor and a rotating shaft with specialized impellers (blades) to induce fluid motion, turbulence, and circulation within a large tank. In many metallurgical processes, such as gold cyanidation, compressed air or oxygen is also injected (sparged) into the slurry. The mechanical action disperses the air into fine bubbles and blends it uniformly throughout the mixture, ensuring high levels of dissolved oxygen needed for the chemical reaction to occur.
The choice of impeller depends heavily on the specific application, slurry density, and required shear rate. Common types include:
Agitators are custom-built for specific conditions. Key design considerations include:
Common problems can lead to reduced efficiency or mechanical failure:
Yes, regular maintenance and periodic inspections are essential for operational longevity. This includes:
Selecting the correct mixer involves assessing several factors related to the material properties and process goals. Key considerations include:
Impellers (blades or paddles) are critical components that determine the flow pattern and mixing intensity. Common types include:
The primary function of an industrial agitator/mixer is to transfer mechanical energy to fluids to blend, disperse, or homogenize materials to a desired consistency. Key objectives include maintaining homogeneity in storage tanks, promoting chemical reactions, suspending solids, facilitating heat transfer, and breaking down agglomerates.