
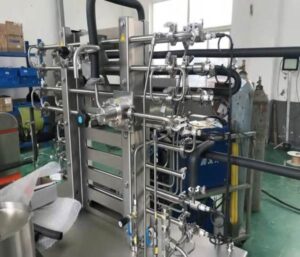
Our Sterilizer is designed for precise thermal processing in research, universities, and pilot-scale production. This compact unit allows teams to simulate thermal treatment and aseptic filling conditions on a small scale before moving to industrial systems. It’s ideal for dairy, beverages, plant-based liquids, sauces, and pharmaceutical liquids requiring controlled heat treatment.
This equipment allows for the accurate processing of new formulas, enabling essential taste testing, product color evaluation, and shelf life testing. With a minimum batch size of just 3 liters, it significantly minimizes material and energy waste during trial runs, making it an efficient development solution. The system achieves standard operating temperatures between 85°C and 150°C for adjustable holding times, facilitating both high-heat and standard HTST processes.
The unit is a self-contained device featuring an integrated steam generator and refrigerator, requiring only electricity and water to operate. It is also built with online Cleaning-In-Place (CIP) and Sterilization-In-Place (SIP) functions, ensuring hygienic operation and fast turnaround between experiments. For complete processing capabilities, the system can be configured with optional components:
Ideal for milk, cream, plant-based milk, juices, and nutritional drinks requiring high-temperature processing.
Used for sauces, soups, condiments, and other liquid foods undergoing pilot trials to evaluate taste, viscosity, and stability.
Suitable for sterile preparations needing controlled thermal simulation before moving to larger production systems.
Recreates full-scale sterilization systems at laboratory size, enabling cost-effective product testing.
Small-batch trials reduce waste and accelerate product development timelines.
Provides consistent performance across multiple validation runs, ensuring dependable data during research.
The device combines precision, flexibility, and ease of use, delivering dependable results for R&D teams. Its capability to handle both HTST and thermal processing makes it a valuable tool for manufacturers, researchers, and formulators looking to refine or scale new liquid products.
We can supply complete systems alongside a Lab UHT production line.
Direct Heating uses steam injection to heat the milk instantly (better flavor, higher cost); Indirect Heating uses heat exchangers (more energy efficient, suitable for most commodity dairy products)
The shelf life for UHT processed milk products typically ranges from six to nine months, provided the product remains sealed in its aseptic packaging.
UHT is better for producing shelf-stable products for ambient storage, while HTST (High-Temperature Short-Time) is better for creating refrigerated, shorter-shelf-life products with minimal flavor change
UHT processing has minimal impact on the major nutritional components of milk, such as protein and minerals. Due to the extremely short holding time (1-10 seconds), loss of heat-sensitive vitamins is also reduced compared to traditional sterilization methods.
The standard operating temperature range for a UHT dairy system is typically 135°C to 150°C with a holding time of just 1 to 10 seconds adjustable